System Overview & Engineering Philosophy
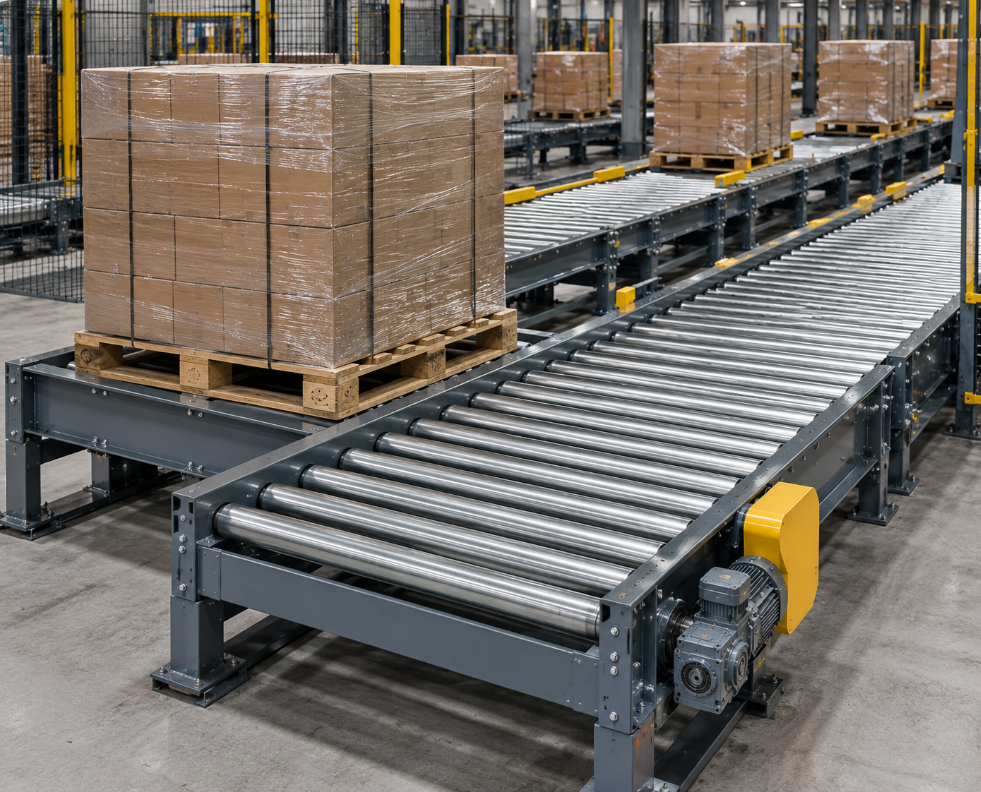
Autorise Empowers Pallet Roller Conveyors are heavy-duty industrial transport systems engineered specifically for the robust, controlled, and automated movement of heavy unit loads, palletized goods, and industrial containers up to 1,500 kg per pallet. Serving as the primary horizontal transport spine connecting production end-of-line packaging, automated palletizers, stretch wrappers, and AS/RS high-bay entry/exit stations, our pallet roller conveyors deliver relentless 24/7 reliability under extreme industrial punishment.
The core engineering philosophy centers on structural over-engineering, torsional rigidity, and intelligent load control. Pallet transport involves massive dynamic inertial forces during acceleration and deceleration. Our conveyor frames utilize heavy-gauge structural channel steel (≥4.5mm thickness) with reinforced cross-tie gussets and heavy floor mounting baseplates that resist forklift impact and eliminate structural sagging. Through zoned zero-pressure accumulation (ZPA) logic, pallets advance sequentially without colliding, preventing fragile product crushing, pallet wood splintering, or unit load destabilization.
Mechanical Architecture & Drive Transmission Mechanics
The roller bed is composed of heavy-wall structural carbon steel rollers (Ø76mm or Ø89mm with 3.0mm to 4.5mm wall thickness) equipped with precision-ground, double-sealed deep groove ball bearings housed in heavy cast steel or machined steel bearing cups. Rollers are electro-galvanized or polyurethane-sleeved for enhanced surface grip and corrosion protection.
Power transmission is executed via precision industrial duplex roller chains in either roll-to-roll loop configurations or continuous tangential chain drives beneath protective steel guard covers. High-efficiency SEW-Eurodrive or Nord helical-bevel gearmotors (0.75 kW to 1.5 kW per zone) provide tremendous starting torque with integrated electromechanical disc brakes for instantaneous hold-in-place positioning. Each conveyor zone features embedded photoelectric retro-reflective sensors and mechanical pallet stops to maintain exact pallet gaps, enabling seamless automatic handoffs to AGVs, shuttles, or vertical elevators.
Key Features & Technological Innovations
- High Payload Capacity: Engineered to transport standard Euro pallets (1200x800mm), industrial GMA pallets (1200x1000mm), and heavy metal skid boxes weighing up to 1,500 kg per unit.
- Zero-Pressure Accumulation (ZPA): Individual motorized zone control prevents pallet-on-pallet collisions, eliminating product damage and ensuring smooth staging queues before AS/RS infeed.
- Heavy-Wall Precision Rollers: Ø76mm / Ø89mm carbon steel rollers with CNC machined spring-loaded hexagonal shafts for effortless maintenance and high torsional strength.
- Bi-Directional Operation: Fully reversible drive control allows dynamic bi-directional routing for flexible pallet staging, sorting, and rejection corridors.
- Integrated Centering & Squaring Guides: Side-mounted structural guide rails and lead-in roller flares automatically correct pallet misalignment before automated strapping or shuttle induction.
- Rugged Modular Construction: Standardized 1.5m, 2.0m, and 3.0m modular lengths allow rapid facility expansion, re-routing, or line extensions with minimal production downtime.
Comprehensive Technical Specifications
- Conveying Speed Range: 12 to 20 m/min (Smooth, controlled transport)
- Maximum Unit Load Capacity: Up to 1,500 kg per pallet (Custom builds up to 2,500 kg)
- Standard Top of Roller (TOR) Height: ≥ 450 mm (Adjustable ±50 mm via heavy-duty leveling feet)
- Roller Specifications: Ø76 mm x 3.0 mm / Ø89 mm x 4.5 mm Hardened Carbon Steel
- Roller Pitch (Spacing): 150 mm / 200 mm (Optimized for 2-way and 4-way pallet entry)
- Drive Motor Type: High-Torque Helical Gearmotor (0.75 kW ~ 1.5 kW, 400V 3-Phase, IP55)
- Transmission Method: Precision Duplex Chain Loop / Tangential Continuous Chain
- Frame Material: Heavy Structural C-Channel Steel (≥4.5 mm thickness, Powder Coated)
- Sensor Array: Polarized Retro-Reflective Photo-Eyes with Heavy Steel Protective Hoods
- Ambient Operating Range: -25°C (Cold Storage) to +45°C (Ambient Industrial)
Operational Benefits & Quantified ROI
Replacing manual forklift transit with automated pallet roller conveyors transforms warehouse throughput, safety, and operating economics. By automating the pallet transfer from production lines to storage grids, facility forklift traffic is reduced by up to 80%, substantially cutting the risk of pedestrian collisions, rack impacts, and equipment maintenance costs. Continuous automated pallet staging eliminates production line bottleneck back-ups, enabling packaging machines to run at maximum rated capacity. Payback on automated pallet conveyor investments is typically achieved within 12 to 18 months through labor reduction, forklift lease cancellations, and dramatic decreases in product breakage.
Industrial Applications & Target Sectors
- Food & Beverage Bottling & Canning: High-speed staging lines from palletizers to automated stretch wrappers and shipping staging.
- Chemical & Petrochemical Drum Packaging: Heavy drum pallet handling, intermediate bulk container (IBC) transit, and hazardous zone staging.
- Heavy Automotive & Machinery Manufacturing: Engine block skid transit, stamped sheet metal pallet transfer, and assembly line feeding.
- Cold Storage & Frozen Food Logistics: Automated pallet infeed airlocks connecting loading docks to -30°C AS/RS shuttle grids.
- Paper, Corrugated & Print Packaging: Heavy paper roll and stacked corrugated pallet handling lines.
Preventative Maintenance Protocols & Chain Lubrication
Our pallet roller conveyors are designed for decades of continuous operation. Scheduled maintenance protocols include monthly checks of drive chain tension and automated chain oiler reservoirs, quarterly torque verification of structural floor anchor bolts, and semi-annual sensor alignment audits to ensure optical beams maintain 100% detection reliability through dusty or washdown environments. Sealed precision bearings eliminate routine re-greasing, while spring-loaded roller shafts allow single-roller replacement in under 2 minutes without dismantling adjacent conveyor frames.
Safety Compliance, Electrical Controls & Enterprise SLA Support
To protect operators in heavy material handling zones, our pallet roller conveyors feature full-length chain guard shrouds, pop-out roller safety brackets, and integrated emergency stop pull-cords. Sensorized muting light curtains allow automated pallet entry into restricted AS/RS airlocks while halting rollers if personnel enter. Control panels utilize Siemens or Allen-Bradley PLCs communicating over PROFINET fieldbus networks with real-time drive diagnostics. Autorise Empowers backs every pallet conveyor installation with comprehensive lifecycle assurance, including emergency spare parts consignment kits, ultrasonic weld testing, and 24/7 on-call field engineering support.
Predictive Telemetry & Real-Time Vibration Monitoring
Every pallet roller conveyor module includes integrated vibration telemetry and bearing temperature monitoring sensors linked to the central SCADA network. By tracking mechanical harmonic frequencies in real time, maintenance teams receive early alerts regarding chain elongation, bearing race degradation, or roller imbalance long before mechanical failure can occur. This predictive intelligence ensures 99.98% operational uptime across high-throughput industrial facilities.