System Overview & Engineering Philosophy
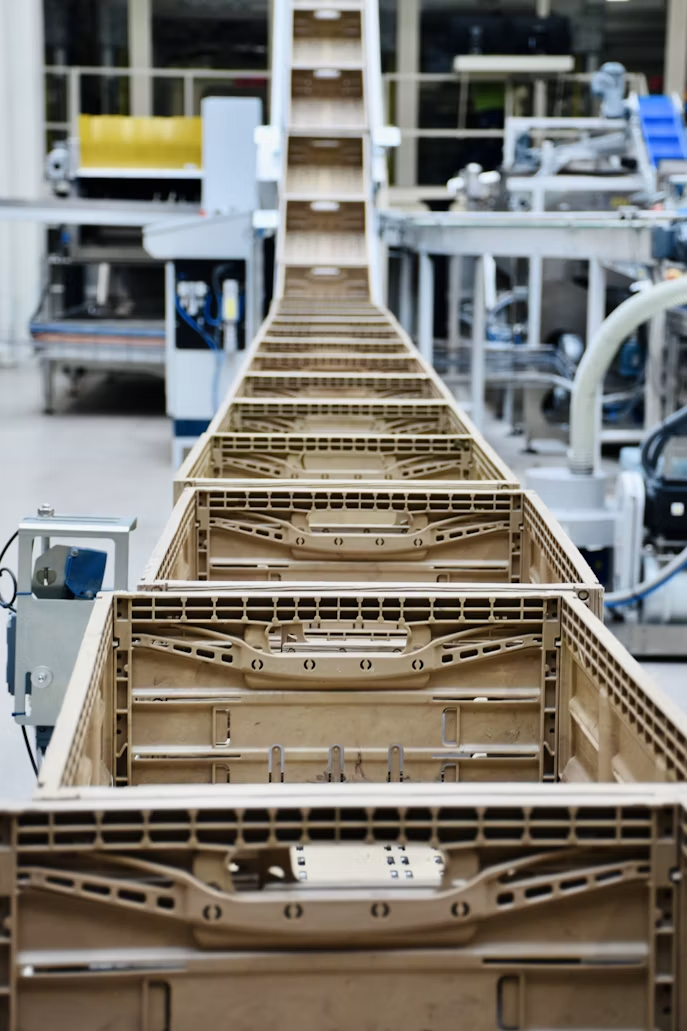
Autorise Empowers Tote Conveyors are high-precision, intelligent material handling networks designed specifically for the rapid, quiet, and energy-efficient transport of plastic tote bins, corrugated cartons, trays, and small parts containers up to 50 kg. Widely utilized in e-commerce fulfillment centers, pharmaceutical order-picking corridors, automated kitting cells, and miniload AS/RS buffer loops, our tote conveyor platforms deliver unmatched operational flexibility and granular control.
The engineering philosophy of our tote conveyor series centers on distributed mechatronic intelligence and "run-on-demand" energy efficiency. Powered by low-voltage 24V or 48V DC Brushless Motorized Drive Rollers (MDR) integrated directly within the conveyor bed, each zone operates independently. Rollers only rotate when a tote is actively entering the zone and immediately enter a dormant sleep state once the container passes. This localized control completely eliminates the energy waste, continuous acoustic noise, and mechanical wear associated with continuously running centralized drive shafts.
Mechanical Architecture & MDR Drive Mechanics
The structural framework is built using precision-extruded anodized aluminum profiles or CNC-bent structural carbon steel side channels with integrated cable management conduits. This sleek, ultra-clean profile eliminates external chain guards, pinch hazards, and exposed wiring harnesses, creating a modern, aesthetically superior industrial appearance suitable for cleanroom and pharmaceutical facilities.
Each conveyor zone consists of one 24V/48V DC brushless motorized drive roller coupled to adjacent slave rollers via high-elasticity Poly-V multi-ribbed belts or reinforced polyurethane O-rings. The Ø50mm precision steel rollers feature carbon steel or stainless steel shafts mounted in vibration-dampening polyamide bearing housings. Dedicated intelligent zone controllers (MDR Controllers) communicate over fieldbus networks (EtherCAT, PROFINET, or AS-i), monitoring motor current, thermal profiles, and photo-eye status to execute complex zero-pressure accumulation (ZPA), singulation, gap control, and speed acceleration curves with millisecond responsiveness.
Key Features & Technological Innovations
- Distributed 24V/48V MDR Technology: Decentralized motorized drive rollers eliminate central drive motors, drive chains, and pneumatic zone brakes.
- Run-On-Demand Energy Efficiency: Consumes up to 60% less electrical power than traditional continuous-run conveyors by powering down idle zones automatically.
- Ultra-Quiet Operation: Stand-alone operational noise levels remain below 60 dB(A), making it ideal for ergonomic operator packing stations and mezzanine pick towers.
- True Zero-Pressure Accumulation (ZPA): Totes advance seamlessly with micro-gapping, completely eliminating product contact, package damage, and container shingling.
- High-Velocity Transit Capabilities: Standard transport speeds from 15 to 35 m/min, with high-speed express bypass zones capable of reaching 60 m/min.
- Modular Plug-and-Play Architecture: Pre-wired modular sections connect via industrial quick-disconnect plugs for ultra-fast installation and flexible reconfiguration.
Comprehensive Technical Specifications
- Conveying Speed Range: 15 to 35 m/min (High-speed express lines up to 60 m/min)
- Maximum Payload Capacity: Up to 50 kg per tote / container
- Roller Diameter: Ø50 mm Precision Carbon Steel (Optional Polyurethane or Rubber Sleeves)
- Usable Conveyor Widths: 400 mm / 600 mm / 800 mm (Matches standard 600x400mm Euro totes)
- Drive System: 24V / 48V DC Brushless Motorized Drive Rollers (MDR) with High-Torque Planetary Gears
- Zone Length: 450 mm to 900 mm per accumulation zone
- Transmission Belts: High-Elasticity Poly-V Multi-Ribbed Belts / Reinforced PU O-Rings
- Chassis Profiles: Anodized Architectural Aluminum Extrusion / Formed Carbon Steel
- Noise Emission: Extremely Low: ≤ 60 dB(A)
- Operating Temperature: 0°C to +45°C (Cold-storage option available down to -20°C)
Operational Benefits & Quantified ROI
Implementing an Autorise Empowers Tote Conveyor network transforms order fulfillment productivity and drastically lowers facility lifecycle operating expenses. In high-density picking zones, automating tote transport to packing stations eliminates thousands of operator walking steps per shift, boosting order picking efficiency by up to 250%. The ultra-quiet MDR architecture creates a comfortable, fatigue-free working environment that enhances operator focus and reduces order picking errors. With zero chain lubrication requirements and minimal moving parts, maintenance labor is reduced by over 70%, yielding complete capital investment payback within 12 to 16 months.
Industrial Applications & Target Sectors
- E-Commerce Order Fulfillment: Goods-to-Person (G2P) pick station loops, tote replenishment lines, and order consolidation buffers.
- Pharmaceutical & Medical Distribution: Cleanroom tote transport, prescription order verification lines, and automated kitting cells.
- Electronics & Semiconductor Assembly: Precision PCB magazine handling, static-safe clean container transfer, and burn-in testing loops.
- Automotive Small Parts Kitting: Sequenced bin delivery to sub-assembly lines and Kanban replenishment corridors.
- Retail & Apparel Micro-Fulfillment: High-speed buffering and routing of order totes to packing and shipping sorters.
Preventative Maintenance Protocols & Zero-Downtime Design
Our tote conveyors are built for virtually maintenance-free operation with zero ongoing oiling or greasing requirements. Individual motorized drive rollers can be swapped in under 5 minutes using quick-release spring-loaded brackets, eliminating lengthy line shutdowns. Poly-V multi-ribbed drive bands feature high tensile modulus, maintaining constant tension over years of multi-shift operation. Integrated LED diagnostic indicators on each zone controller provide instant visual feedback on power supply voltage, photo-eye alignment, and motor overcurrent status.
Safety Standards, Electrical Fieldbuses & Enterprise SLA
Tote conveyors operate on intrinsically safe low-voltage 24V/48V DC power, eliminating high-voltage electrical hazards along operator workstations. Emergency stop pushbuttons at pick stations instantly disconnect motor bus power. The distributed control architecture communicates with host WCS systems via EtherCAT, PROFINET, or Ethernet/IP, providing real-time tote tracking and dynamic routing decisions. Autorise Empowers provides complete lifecycle assurance under our enterprise SLA frameworks, including remote bus diagnostic monitoring, predictive MDR motor life algorithms, replacement parts consignment packages, and 24/7 on-call technical support.
Intelligent Zone Controller Network & Decentralized Logic
The distributed MDR architecture utilizes high-speed Ethernet fieldbuses allowing each conveyor zone to act as an autonomous decision node. If downstream zones become congested, upstream controllers automatically execute dynamic zero-pressure queuing without waiting for central PLC polling cycles. This decentralized intelligence reduces network bandwidth usage, eliminates communication bottlenecks, and ensures instantaneous response times during high-velocity carton induction sequences.